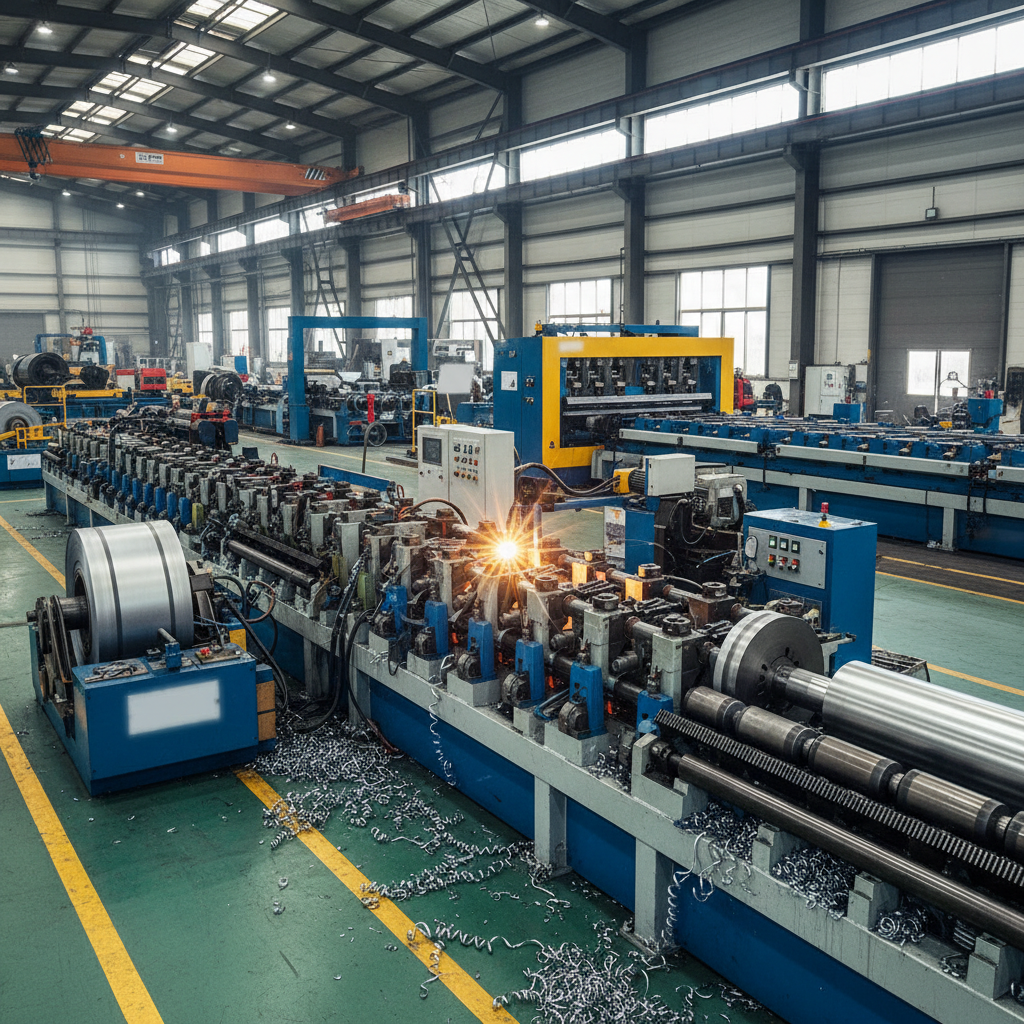
The modernization of metal fabrication depends heavily on the efficiency of High-Frequency Induction (HFI) welding, where precision components like the impeder play a critical role. While the industry often looks for an automatic package machine to handle the final stages of production, the core quality of the pipe is determined by how the electromagnetic field is concentrated during the welding process. Understanding the synergy between high-performance components and automated systems is essential for maximizing throughput in any modern tube mill.
Global demand for carbon steel and stainless steel piping is rising, pushing manufacturers to seek ways to reduce energy loss and improve weld consistency. The integration of ferrite core impeders allows for significant power savings and higher welding speeds, creating a streamlined workflow that often precedes the final stages handled by an automatic package machine. By optimizing the heat distribution at the weld seam, factories can ensure that the output meets international ISO standards for durability and structural integrity.
For professionals managing ERW pipe production, the transition from raw coil to finished product requires a series of specialized auxiliary machines. Whether you are optimizing your welding efficiency or searching for a reliable automatic package machine to secure your finished goods, the focus remains on reducing waste and increasing precision. This guide explores the technical specifications of the impeder and its vital role in the broader manufacturing ecosystem.
The Role of Impeder in ERW Tube Welding
The impeder is a fundamental component in High-Frequency Induction (HFI) welding lines, serving as the guide that concentrates the electromagnetic field precisely around the weld area. Without a high-quality impeder, the induction current would disperse throughout the pipe body, leading to massive energy waste and uneven heating of the edges. This concentration is what allows the ERW (Electric Resistance Welding) process to achieve the high speeds required for industrial-scale production.
By utilizing premium manganese-zinc (MnZn) ferrite rods, these components ensure that the magnetic flux is maximized while power loss is minimized. This level of precision is what enables the production of everything from thin-wall precision pipes to heavy-duty carbon steel tubes. Once these pipes are welded and sized, they are often moved via conveyors toward an automatic package machine for final bundling and shipping.
Key Functions and High Magnetic Efficiency
At the heart of the impeder's functionality is the ability to create a high-intensity magnetic field in a very localized zone. This is achieved through the use of high-grade MnZn ferrite, which possesses the necessary magnetic permeability to drive the current to the pipe's edges efficiently. This process ensures that the weld seam reaches the necessary forging temperature rapidly and uniformly, regardless of the material's thickness.
Beyond mere heating, the impeder prevents the "skin effect" from dispersing the energy across the entire surface of the tube. By guiding the current, it reduces the overall electrical load on the HF welder, which not only extends the life of the power source but also lowers the cost per meter of pipe produced. This efficiency is a prerequisite for any facility that aims to integrate downstream automation, such as an automatic package machine.
Customization is another key factor; since different pipe diameters (ranging from 10mm to 325mm) require different magnetic flux densities, the configuration of the ferrite rods—whether single, multi-rod, or split-core—must be precisely engineered. This bespoke approach ensures that the welding intensity is perfectly matched to the specific grade of steel being processed.
Cooling Systems and Ferrite Longevity
Thermal management is the most significant challenge when operating high-power welding lines. Because the impeder operates in close proximity to the intense heat of the weld seam, overheating can lead to ferrite cracking and catastrophic failure. To combat this, AIS MACHINERY provides both water-cooled and air-cooled options to maintain stable operating temperatures.
Internal water circulation is the gold standard for high-speed lines exceeding 200 kW. By circulating coolant directly through the core, the system prevents the ferrite from reaching its Curie temperature, which would otherwise cause it to lose its magnetic properties. This reliability ensures that the production line remains active, providing a steady flow of products for the automatic package machine at the end of the line.
For smaller operations or lower-speed production of precision tubes, air-cooled impeders offer a simpler, maintenance-free alternative. Regardless of the cooling method, the use of heat-resistant composite or stainless steel outer casings protects the sensitive ferrite rods from mechanical impact and corrosive environments, extending the overall service life of the component.
Technical Parameters for Optimal Performance
Selecting the correct impeder requires a deep understanding of the relationship between welding power, pipe diameter, and production speed. A mismatched impeder can result in "cold welds" or excessive energy consumption, which disrupts the entire production cadence. The technical specifications must be aligned with the HF welder's output to ensure the most efficient conversion of electrical energy to heat.
From the rod diameter (typically 6–25 mm) to the total length (up to 1000 mm), every dimension affects the magnetic flux concentration. When these parameters are optimized, the efficiency of the welding process increases by 15–25%, significantly reducing the operational overhead of the mill before the final stage of the automatic package machine.
Efficiency Rating of Impeder Configurations
Global Applications in Pipe Manufacturing
The application of high-performance impeders spans across diverse industrial sectors globally, from the construction of skyscrapers in Asia to the oil and gas infrastructure in North America. In these regions, the ability to produce galvanized and stainless steel pipes with high consistency is paramount. The impeder ensures that the metallurgical bond of the weld is strong enough to withstand high-pressure environments.
Furthermore, in the manufacturing of thin-wall precision pipes, where the margin for error is nearly zero, the impeder's ability to concentrate heat without distorting the pipe shape is critical. Once these precision tubes are produced, they are often bundled using an automatic package machine to ensure they reach the client without surface damage or deformation.
Energy Savings and Operational Value
The financial impact of using a high-efficiency impeder is most evident in the energy bills of a large-scale pipe mill. By improving welding efficiency by up to 25%, manufacturers can significantly reduce the kW per ton of steel produced. This not only lowers costs but also aligns the factory with global sustainability goals by reducing the overall carbon footprint of the fabrication process.
Operational value is also found in the reduction of scrap rates. When the heat is concentrated correctly, the occurrence of "burn-through" or incomplete welds is minimized. This leads to a higher percentage of first-pass quality products, which optimizes the utilization of downstream equipment like the automatic package machine, as there are fewer rejects to sort.
Moreover, the use of CNC-positioned key grooves and high-precision rollers in the surrounding machinery ensures that the impeder remains perfectly aligned. This stability reduces mechanical vibration and noise, creating a safer and more productive working environment for the operators.
Maintenance and Replacement Strategies
Due to the harsh conditions of ERW welding, impeders are considered wear parts with a typical service life of 6 to 12 months. Regular inspection of the ferrite rods for micro-cracks and the verification of water-cooling seal integrity are essential to prevent unplanned downtime. A proactive replacement strategy ensures that the production line never halts unexpectedly.
AIS MACHINERY simplifies this process by offering separate replacement ferrite rods in various diameters and lengths. This allows operators to perform "core-only" replacements without needing to replace the entire outer casing, reducing both cost and waste. Efficient maintenance routines ensure that the pipeline of products flowing into the automatic package machine remains uninterrupted.
The use of quick-plug and flanged connections further reduces the time required for installation. By minimizing the Mean Time to Repair (MTTR), factories can maintain higher Overall Equipment Effectiveness (OEE), ensuring that the investment in both the welding line and the final automatic package machine delivers maximum ROI.
Analysis of Impeder Specifications and Service Life
| Impeder Type |
Cooling Method |
Expected Life |
Power Range |
| Standard Water-Cooled |
Internal Water |
8-12 Months |
200-1200 kW |
| Precision Air-Cooled |
External Air |
6-10 Months |
60-200 kW |
| Custom Split-Core |
Internal Water |
10-12 Months |
400-1000 kW |
| Heavy-Duty MnZn |
Internal Water |
12 Months+ |
600-1200 kW |
| Small Diameter Core |
Air/Water Hybrid |
6-8 Months |
60-150 kW |
| Stainless Casing Model |
Internal Water |
9-12 Months |
200-800 kW |
FAQS
Selection primarily depends on the pipe diameter (ranging from 10mm to 325mm), the total welding power of your HF welder, and the desired production speed. A larger pipe diameter typically requires a longer impeder with a larger ferrite rod diameter to ensure the magnetic flux is sufficient to heat the edges. AIS MACHINERY engineers can analyze your specific line configuration to recommend the optimal diameter, length, and core type (single vs. multi-rod) to maximize efficiency.
The main difference is the heat dissipation capacity. Water-cooled impeders use internal water circulation to remove heat rapidly, making them essential for high-speed, high-power welding (above 200 kW) where the ferrite would otherwise overheat and crack. Air-cooled types are simpler and more cost-effective, suitable for smaller pipe production or lower-speed lines where the heat generated is manageable through natural or forced air convection.
Generally, impeders should be replaced every 6 to 12 months. The actual lifespan depends on several factors: the quality of the cooling water (to prevent scaling), the average welding temperature, and the overall wear on the ferrite rods. We recommend a monthly inspection of the ferrite cores and seals to detect micro-cracks early, ensuring the line continues to feed the automatic package machine without interruption.
Yes, AIS MACHINERY supplies replacement ferrite rods in various diameters (6–25 mm) and lengths (200–1000 mm) to fit all standard impeder models. This allows operators to replace only the worn-out magnetic core while retaining the brass, stainless steel, or composite outer casing, which significantly reduces maintenance costs and reduces material waste during the replacement process.
Absolutely. We provide full OEM and custom-made impeder designs to match your specific pipe mill configuration, power source, and coil design. Whether you need a split-core design for easier installation or a specific rod configuration for thin-wall precision tubes, our technical team can engineer a solution that optimizes magnetic flux for your unique production requirements.
The impeder acts as a magnetic lens, focusing the induction current exactly where it is needed—at the weld seam. By preventing the energy from leaking into the body of the pipe, it reduces the power required to reach the welding temperature. This typically results in an energy saving of 15% to 25%, which, when scaled across thousands of tons of pipe, results in substantial operational cost reductions.
Conclusion
The impeder is an unsung hero of the ERW tube welding process, transforming an inefficient induction field into a precise heating tool. By focusing on high-grade MnZn ferrite materials and advanced cooling systems, manufacturers can achieve superior weld quality, reduce energy consumption by up to 25%, and ensure a consistent flow of high-quality pipes. When paired with the right auxiliary equipment and a final automatic package machine, the entire production line becomes a model of industrial efficiency.
As the industry moves toward further automation and green manufacturing, the role of optimized components will only grow. We encourage mill operators to regularly audit their welding efficiency and consider customized impeder solutions to stay competitive. For those looking to upgrade their ERW lines or integrate high-precision auxiliary machines, visiting our website is the first step toward operational excellence. Visit our website: www.aistubemill.com
 Tel:86-15176910262