-
 Tel:86-15176910262
-

Search
 Tel:86-15176910262
Search
High Frequency Welding (HF Welding) is one of the most important processes in an Electric Resistance Welded (ERW) tube mill. It joins the edges of a continuously formed steel strip to produce a strong, continuous longitudinal weld.
Modern ERW tube mills use high-frequency electrical energy to heat the strip edges to the required welding temperature. The heated edges are then pressed together by squeeze rolls, creating a metallurgical bond without the need for additional welding filler material.
Understanding how HF welding works is essential when selecting an ERW tube mill, HF welder, impeder, and other welding components.
In this article, we explain the working principle of high-frequency welding, the main components of an ERW welding system, common welding problems, and the key factors that affect weld quality.
High Frequency Welding is a resistance welding process used to join the edges of steel strip during ERW tube production.
Unlike conventional arc welding, HF welding does not use welding wire or electrodes to fill the joint. Instead, high-frequency electrical current heats the edges of the steel strip, and mechanical pressure from squeeze rolls completes the weld.

The basic process is:
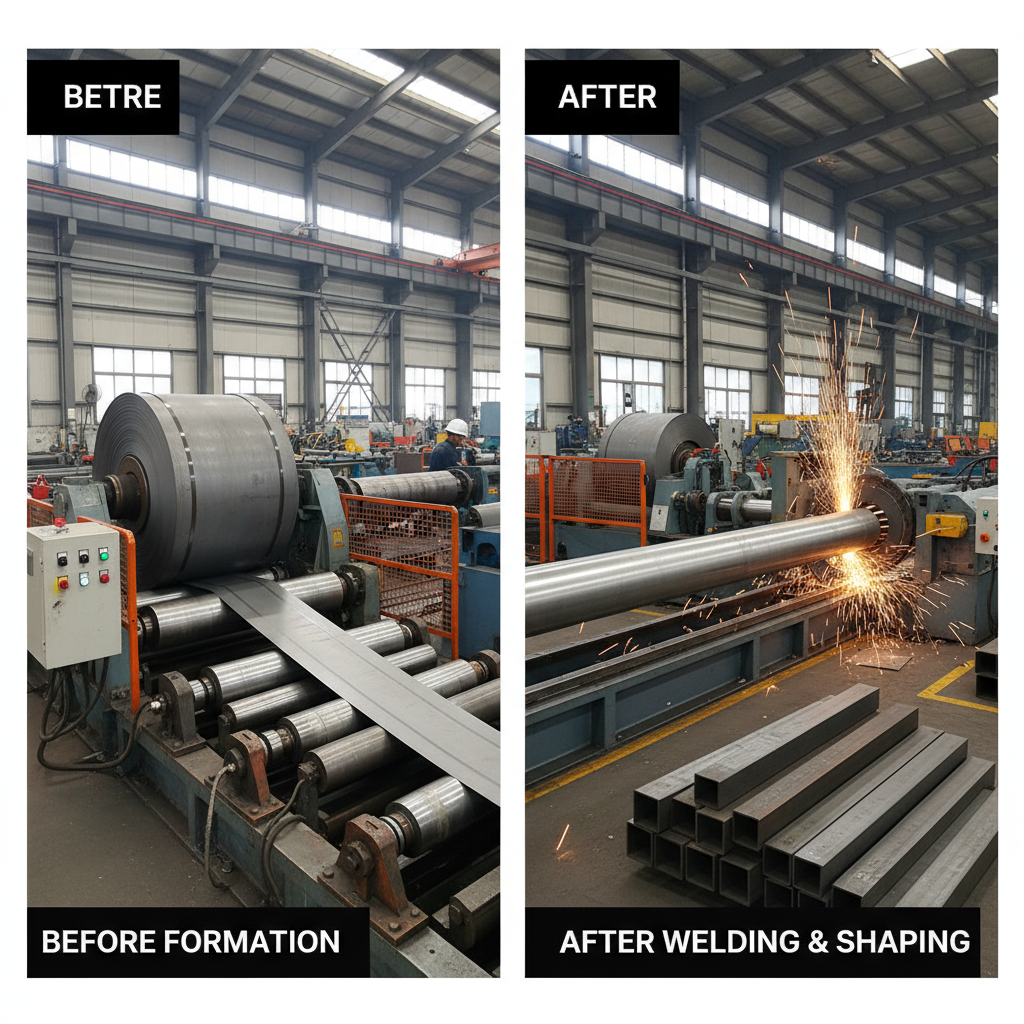
Steel Strip → Forming → Edge Heating → Edge Joining → Squeeze Rolls → Welded Tube
HF welding is commonly used for manufacturing:
Carbon steel tubes
Stainless steel tubes
Galvanized steel tubes
Structural tubes
Mechanical tubing
Automotive tubes
API and oil & gas pipes
Solar mounting tubes
The HF welding process can be divided into several stages.
The process begins with a steel coil.
The uncoiler feeds the strip into the forming section of the ERW tube mill. Multiple forming stands gradually bend the flat strip into a round or near-round tubular shape.
At the welding point, the two longitudinal edges of the strip are positioned close together.
The quality of this forming process is extremely important because poor edge alignment can directly affect weld quality.

Once the strip reaches the welding section, a high-frequency current is introduced into the steel.
The current flows along the edges that need to be joined.
Because the electrical resistance of the steel generates heat, the temperature of the strip edges rapidly increases.
The objective is to heat the edges to the appropriate welding temperature without unnecessarily heating the entire tube.
This concentrated heating is one of the major advantages of HF welding.
At high frequencies, electrical current tends to concentrate near the surface of a conductor. This phenomenon is known as the skin effect.
The skin effect allows HF current to concentrate near the tube edges, making the heating process much more efficient than conventional low-frequency resistance heating.
In ERW tube production, the frequency and electrical characteristics of the material affect how the current is distributed and how quickly the edges are heated.
The proximity effect is another important phenomenon in HF welding.
When the two edges of the strip are positioned close to each other, the electromagnetic field causes the HF current to concentrate around the edges that are being joined.
This helps deliver electrical energy directly to the welding zone.
The combination of the skin effect and proximity effect allows HF welding systems to achieve high production speeds while concentrating heat where it is needed.
The impeder is an important component inside the tube during HF welding.
Its primary function is to increase the electrical impedance of the unwanted current path through the inside of the tube and help direct the HF current toward the strip edges.
A typical impeder assembly includes:
Ferrite rods
Impeder core
Cooling system
Impeder housing
The impeder must be correctly selected according to:
Tube diameter
Wall thickness
Steel grade
Welding frequency
Production speed
An incorrectly selected or poorly cooled impeder can significantly reduce welding efficiency.

As the HF current flows through the strip edges, electrical resistance generates heat.
The temperature at the edges rises rapidly.
The heating level depends on several factors, including:
Welding power
Welding frequency
Line speed
Material grade
Strip thickness
Tube diameter
Edge condition
Forming quality
The objective is to achieve sufficient edge heating for welding while avoiding excessive overheating.
After the edges reach the appropriate welding temperature, the strip passes through the squeeze rolls.
The squeeze rolls apply pressure to force the heated edges together.
This produces a continuous metallurgical bond.
The squeeze rolls therefore play a critical role in determining final weld quality.
If the squeeze pressure is too low, incomplete bonding or lack of fusion may occur.
If the pressure is excessive, too much material may be expelled from the weld zone and the weld geometry may become undesirable.
During welding, a small amount of heated material is expelled from the weld area.
This creates the characteristic weld bead.
Depending on the application, the external weld bead may be removed by an online bead scarfing system.
For certain tube applications, internal bead removal may also be required.
The final requirements depend on:
Tube application
Customer specifications
Applicable standards
Wall thickness
Surface requirements
A complete HF welding system normally includes several major components.
The HF welder converts electrical energy into high-frequency power suitable for tube welding.
Modern solid-state HF welders commonly use semiconductor technology such as MOSFET or IGBT-based power modules, depending on the system design and power range.
The HF welder controls the welding power supplied to the tube mill.
The induction coil transfers high-frequency electrical energy to the tube.
Its design affects the efficiency and stability of the welding process.
Important factors include:
Coil geometry
Distance from the tube
Tube diameter
Material
Welding frequency
Cooling

The impeder helps concentrate HF current around the tube edges and reduces unwanted current flow through the interior of the tube.
Ferrite materials are commonly used because of their electromagnetic properties.
Proper impeder selection is particularly important for high-speed tube production.

Squeeze rolls bring the heated strip edges together and provide the mechanical pressure required to complete the weld.
The roll position, alignment, and pressure must be properly adjusted.
The control system monitors and adjusts important parameters such as:
Welding power
Line speed
Current
Voltage
Frequency
Cooling conditions
Welding stability
Modern ERW tube mills can integrate the HF welding system with the main PLC and production control system.
HF welding systems operate at frequencies much higher than conventional power-frequency electrical systems.
Common industrial tube-welding frequencies can range from tens to hundreds of kilohertz, depending on the machine design, material, tube size, wall thickness, and welding requirements.
The optimum frequency is not determined by one factor alone.
A professional HF welding system should be matched to the complete tube mill configuration rather than selected only according to maximum output power.
One of the most important questions when selecting an ERW tube mill is:
How much HF welding power is required?
There is no single power value suitable for every tube size.
Required welding power depends on:
Larger tubes generally require more welding energy.
Thicker materials require greater heat input to bring the edges to the required welding condition.
As line speed increases, the available heating time decreases.
Therefore, higher production speeds generally require higher welding power.
Different steel grades have different electrical and thermal properties.
The design of the induction coil, impeder, welding section, and HF welder affects overall energy efficiency.
Even with a high-quality HF welder, incorrect process parameters can result in welding defects.
Lack of fusion occurs when the edges do not reach the required welding condition or sufficient pressure is not applied.
Possible causes include:
Insufficient welding power
Excessive line speed
Incorrect squeeze pressure
Poor edge preparation
Incorrect coil position
Weld cracking can be caused by inappropriate welding parameters, material characteristics, excessive cooling, or poor forming conditions.
The exact cause should be investigated through the complete welding and forming process rather than adjusting HF power alone.
An excessive weld bead may indicate unsuitable welding conditions or squeeze pressure.
The bead scarfing system may also require adjustment.
Welding instability may result from:
Fluctuating power
Incorrect coil alignment
Poor tube forming
Impeder problems
Inconsistent material
Cooling problems
Incorrect welding parameters
To achieve stable weld quality, manufacturers should control the complete production process.
The strip edges must meet consistently at the welding point.
Poor alignment can lead to unstable welding and inconsistent weld penetration.
Ferrite components can become damaged if the impeder temperature becomes excessive.
Adequate cooling is therefore essential for stable production.
The coil must be matched to the tube diameter and production requirements.
Incorrect coil positioning can reduce heating efficiency.
Increasing line speed without sufficient welding power can result in insufficient edge heating.
Conversely, excessive power can cause overheating and unstable welding.
Squeeze roll pressure should be carefully adjusted according to the tube specification and material.
HF welding provides several important advantages for continuous tube production.
| Feature | HF Welding | Conventional Arc Welding |
|---|---|---|
| Welding Speed | Very High | Lower |
| Filler Material | Not normally required | Usually required |
| Continuous Production | Excellent | Good |
| Heat-Affected Area | Relatively Narrow | Generally Larger |
| Automation | Excellent | Good |
| Production Efficiency | High | Moderate |
| Application | ERW Tube Mills | Fabrication & other applications |
For high-volume steel tube manufacturing, HF welding is particularly attractive because it can operate continuously at high production speeds.
Modern ERW tube mills increasingly use solid-state HF welding technology.
Compared with older vacuum-tube-based systems, modern solid-state systems can provide:
High energy efficiency
Stable output
Compact design
Easier maintenance
Fast response
High automation
Improved operational reliability
The exact power configuration should be selected according to the tube size, thickness, material, and required production speed.
When selecting an HF welder, don't simply choose the largest available power rating.
Consider the following:
Maximum tube diameter
Minimum tube diameter
Maximum wall thickness
Minimum wall thickness
Steel grade
Production speed
Welding frequency
Required production capacity
Cooling system
Impeder and coil configuration
A properly matched welding system can improve both production efficiency and weld quality.
The complete process can be summarized as:
1. Steel Coil
↓
2. Uncoiling
↓
3. Strip Flattening
↓
4. Forming
↓
5. HF Edge Heating
↓
6. Squeeze Welding
↓
7. Weld Bead Removal
↓
8. Cooling
↓
9. Sizing
↓
10. Cutting
↓
11. Inspection
↓
12. Finished Tube
HF welding is therefore only one part of the complete ERW tube manufacturing process. Forming accuracy, welding parameters, cooling, sizing, and cutting all contribute to the final tube quality.
The welding section is often considered the heart of an ERW tube mill.
A high-quality HF welding system can help manufacturers achieve:
Stable weld quality
High production speeds
Lower energy consumption
Reduced production downtime
Consistent tube performance
Better overall production efficiency
However, the HF welder itself cannot compensate for poor forming, incorrect roll design, poor strip quality, or improper welding setup.
The entire tube mill must be designed and configured as an integrated production system.
When purchasing an ERW tube mill, it is important to evaluate the entire production line rather than selecting individual components separately.
A complete solution may include:
Uncoiler
Shear & End Welder
Accumulator
Forming Mill
HF Welder
Induction Coil
Impeder
Squeeze Rolls
Cooling System
Sizing Section
Cutting Machine
Online Inspection Equipment
PLC Control System
At HEBEI AIS MACHINERY, we provide complete ERW tube mill solutions based on tube size, wall thickness, material, production speed, and customer requirements.
Our engineering team can help customers select the appropriate forming technology, HF welding system, impeder, induction coil, sizing section, and cutting solution for their production requirements.
High Frequency Welding is a highly efficient technology for continuously joining steel strip edges in ERW tube production.
The process uses high-frequency electrical energy to heat the strip edges, while squeeze rolls apply pressure to complete the weld. The skin effect, proximity effect, induction coil, impeder, and squeeze rolls all play important roles in achieving stable welding performance.
For manufacturers investing in an ERW tube mill, understanding HF welding is essential for selecting the right equipment and achieving the required production speed and weld quality.
A properly designed HF welding system, combined with accurate forming, effective cooling, correct impeder selection, and precise process control, can provide reliable and efficient ERW tube production for a wide range of industrial applications.
HF welding means High Frequency Welding. It uses high-frequency electrical energy to heat the edges of steel strip before they are pressed together to form a continuous weld.
HF welding is one of the main welding technologies used in modern ERW tube mills. The term ERW describes the broader electric resistance welding process.
No. HF welding normally joins the strip edges without adding welding filler wire.
An impeder helps control the HF current path and concentrate electrical energy around the strip edges, improving welding efficiency.
Welding power determines how much electrical energy can be delivered to the strip edges. It must be matched with tube size, wall thickness, material, and production speed.
Yes. HF welding can be used for various conductive metals, including stainless steel, provided the welding system and process parameters are properly designed for the material.
The HF welder should be selected based on the complete tube mill requirements, including tube diameter, wall thickness, steel grade, production speed, and required welding power.
How Does High Frequency Welding Work in ERW Tube Mills?
Learn how high frequency welding works in ERW tube mills, including HF welders, induction coils, impeders, squeeze rolls, welding power, and common welding defects.
/how-high-frequency-welding-works-erw-tube-mills
High Frequency Welding
HF Welding
HF Welder
ERW Tube Mill
ERW Welding
High Frequency Welder
Tube Mill Welding
HF Welding Machine
ERW Tube Welding
Tube Mill HF Welder
High Frequency Welding Machine
Looking for a complete understanding of ERW TUBE MILL technology? Read our Ultimate Guide to ERW TUBE MILL.
Looking for a complete understanding of steel coil slitting technology? Read our Ultimate Guide to Steel Coil Slitting Line.
Send a Message
Dear customer, thank you for your attention! We provide high-quality machinery and equipment and look forward to your orders. Please inform us of your needs and we will respond quickly!