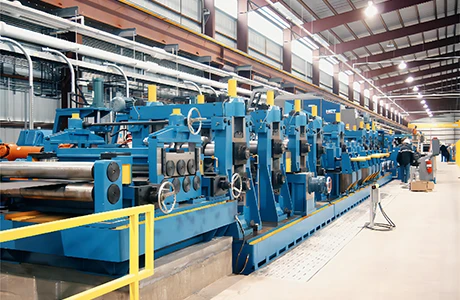
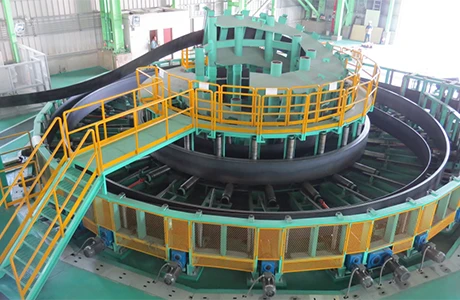
In the high-precision world of ERW tube mill production, maintaining a continuous flow of material is critical to maximizing throughput and reducing waste. The cage accumulator, often referred to in technical circles as a cage loop, serves as the essential buffer that bridges the gap between the uncoiler and the forming mill. By storing the steel strip helically, it allows the production line to keep running even when the coil is being changed or the welder is in operation.
The global demand for high-quality steel piping in construction, automotive, and energy sectors has pushed manufacturers to seek more reliable material handling solutions. Without an efficient storage system, any interruption at the front end of the line causes an immediate stop at the forming and sizing sections, leading to significant downtime and potential material defects. Implementing a robust cage loop system ensures that the forming mill operates at a constant speed, which is the primary driver of product consistency.
Understanding the technical nuances of the cage loop is vital for plant managers looking to optimize their ROI. From managing strip tension to selecting the right frame reinforcement for heavy-duty alloys, the right configuration can increase overall line efficiency by eliminating unnecessary stoppages. This guide explores the engineering, application, and strategic advantages of integrating these systems into modern tube mill architectures.
The Fundamental Role of Cage Loop in Production
The cage loop acts as a sophisticated reservoir for steel strips within an ERW tube mill line. By storing the material helically around a vertical frame, it creates a buffer that decouples the intermittent feeding process of the uncoiler and shear-welder from the continuous demand of the forming mill. This ensures that the mill never runs dry, which is critical for maintaining the thermal stability of the welding process.
Beyond simple storage, this system is engineered to maintain precise strip tension. If the tension fluctuates, the resulting steel pipes may suffer from camber or uneven wall thickness. Therefore, the cage loop is not just a convenience but a quality-control component that ensures the raw material enters the forming section in a perfectly controlled state, regardless of the upstream activities.
Core Technical Requirements for Stability
To ensure vibration-free operation at speeds up to 120m/min, the structural integrity of the cage frame is paramount. High-strength welded structures are mandatory, typically treated with shot blasting and anti-corrosion coatings to withstand the harsh environment of a steel mill. Any structural instability can lead to oscillations that compromise the strip's path and increase the risk of surface scratching.
Precision in the rotating components is equally critical. The use of imported bearings for key rotating parts ensures that the helical movement remains smooth and stable. This mechanical precision reduces friction and wear, extending the lifespan of the equipment while ensuring that the strip flows seamlessly without sudden jerks or tension spikes.
Safety is the final pillar of technical design. Modern systems must integrate anti-strip-jumping devices to prevent the material from leaping off the frame during high-speed transitions. Coupled with CE-standard emergency stop systems and protective fencing, these features ensure that the high-energy environment of the production line remains safe for operators.
Application Solutions for Different Capacities
For standard production lines, the typical workflow involves an uncoiler, shear and butt welder, and then the cage loop before the strip enters the forming mill. This basic configuration is ideal for medium-capacity requirements where the focus is on reliable, consistent output for carbon steel or stainless steel pipes.
High-speed upgrades transform the process through the integration of PLC-based speed control and automatic uncoilers. By synchronizing the cage loop with the rest of the line, manufacturers can achieve fully automated production, reducing human intervention and maximizing the efficiency of double-head shear and butt welders.
When dealing with high-strength steel strips—specifically those with thicknesses between 3.0mm and 4.5mm—a heavy-duty solution is required. This involves a reinforced cage frame paired with a servo-controlled tension system, ensuring that the immense force of the thicker material does not deform the frame or cause strip breakage during acceleration.
Comparing Cage Loop and Disk Accumulators
When choosing between a cage loop and a disk accumulator, the primary considerations are cost, speed, and available floor space. Cage accumulators are generally more cost-effective, often costing about 20% less than disk versions because they rely more on mechanical simplicity than complex, heavy-duty drive systems.
While disk accumulators are superior for ultra-high-speed lines exceeding 150m/min, the cage system is the optimal choice for the vast majority of standard ERW mills. It provides a moderate footprint, saving roughly 30% of space compared to traditional horizontal accumulators, making it ideal for factories with limited overhead or floor area.
Operational Efficiency Comparison of Accumulator Types
Key Advantages of Helical Material Storage
The most immediate advantage of the cage loop is its balance of simplicity and performance. Because it utilizes a natural helical storage pattern, it ensures uniform strip tension across the entire stored length. This minimizes the risk of forming defects, such as wrinkles or uneven stresses, which often occur in less stable buffering systems.
From a maintenance perspective, the cage system is far more accessible. Being primarily composed of high-strength mechanical parts, it requires significantly less specialized servicing than servo-heavy disk systems. This lower complexity translates to reduced operational costs and less downtime for routine inspections, ensuring the production line remains active.
Future Trends in Automated Tension Control
As industry 4.0 penetrates the metalworking sector, the cage loop is evolving from a passive mechanical buffer into an intelligent, sensing component. The integration of real-time tension sensors and AI-driven feedback loops allows the system to adjust its feeding speed instantaneously, compensating for any variations in the incoming strip thickness or material elasticity.
Digital transformation is also influencing the materials used in construction. We are seeing a shift toward ultra-lightweight, high-strength alloys for the cage frame, which reduce the inertia of the system. This allows for faster acceleration and deceleration cycles, further increasing the maximum strip speed and improving the overall agility of the ERW tube mill.
Furthermore, the push for "green" manufacturing is leading to the development of energy-efficient drive systems. New pneumatic and electric hybrid controls are reducing the power consumption of the accumulator by optimizing the torque applied during the storage and release phases, aligning production goals with global sustainability standards.
Selection Guide for Optimized Performance
Selecting the right cage loop depends primarily on the strip width and thickness of the target product. For strips under 200mm, a light-duty accumulator with a storage capacity of 100-150 meters is usually sufficient. However, for widths exceeding 400mm, a reinforced heavy-duty structure is necessary to prevent frame deflection under the weight of the stored steel.
Line speed is the second critical factor. If the production line operates below 80m/min, standard mechanical safety devices are adequate. Once speeds climb toward 120m/min, it becomes imperative to install enhanced anti-strip-jumping systems and emergency braking to ensure operational safety and prevent catastrophic material failure.
Finally, specific material requirements, such as the production of stainless steel, necessitate a non-contact strip guiding system. This prevents surface scratching and maintains the aesthetic quality of the finish. By balancing these technical requirements against factory floor constraints, manufacturers can customize a solution that maximizes both output and quality.
Technical Configuration Guide for Cage Loop Selection
| Strip Width Range |
Recommended Model |
Storage Capacity |
Tension Control |
| ≤ 200mm |
Light Duty Cage |
100–150m |
Pneumatic |
| 200–400mm |
Medium Duty Cage |
150–200m |
Electric/PLC |
| ≥ 400mm |
Heavy Duty Cage |
200m+ |
Servo-Controlled |
| 0.5–2.0mm Thickness |
Standard Config |
Customizable |
Conventional Motor |
| 2.0–4.5mm Thickness |
Reinforced Frame |
Customizable |
High-Response System |
| Stainless Steel |
Surface Protect Model |
Standard |
Non-contact Guiding |
FAQS
The primary difference lies in cost, speed, and complexity. A cage loop is more cost-effective (roughly 20% cheaper) and easier to maintain due to its mechanical nature. However, disk accumulators are designed for ultra-high-speed production (above 150m/min), whereas cage loops are ideal for medium-to-high speed ERW mills (up to 120m/min). Additionally, cage loops generally offer a smaller footprint, saving about 30% of factory space.
Yes, but it requires a Heavy-Duty Solution. For strips between 3.0mm and 4.5mm, we recommend a reinforced cage frame to prevent structural deformation and a servo-controlled tension system. This ensures the system can handle the increased load and maintain stable strip tension without causing breakage or frame vibration.
Safety is integrated through the installation of anti-strip-jumping devices and reinforced guardrails. These mechanical barriers keep the strip aligned within the helical path. For lines running between 80-120m/min, we further recommend emergency braking systems and limit switches to stop the machine instantly if an anomaly is detected.
Absolutely. For stainless steel, which is highly sensitive to surface scratches, we provide a specialized non-contact strip guiding system. This ensures that the material is buffered and fed into the forming mill without any abrasive contact, preserving the high-quality surface finish required for stainless steel products.
Maintenance is relatively simple compared to other accumulators. It mainly involves the lubrication of imported bearings and the inspection of the welded frame for wear. Because it consists mostly of mechanical parts, routine servicing is low-cost and can be performed quickly by on-site technicians without needing specialized servo-system engineers.
Capacity depends on your strip width and the frequency of coil changes. Typically, small-size units offer 100-150m, standard units 150-200m, and large-size units 200m+. You should calculate the time required for your shear and butt welder to complete a joint; the cage loop must hold enough material to keep the forming mill running during that entire interval.
Conclusion
In summary, the cage loop is an indispensable component for any ERW tube mill aiming for a balance of cost-efficiency and high productivity. By providing a reliable buffer and maintaining precise tension, it eliminates production gaps and ensures the structural integrity of the final pipe. Whether through standard mechanical configurations or high-speed PLC-integrated upgrades, the cage accumulator optimizes the flow from the uncoiler to the forming mill, significantly reducing downtime and operational waste.
Looking ahead, the integration of smart sensing and sustainable drive systems will continue to enhance the capabilities of helical storage. For manufacturers, the key to success lies in matching the accumulator's specifications—such as frame strength and tension control—to their specific material and speed requirements. We invite you to explore our full range of entry-section equipment to further optimize your production line. Visit our website: www.aistubemill.com
 Tel:86-15176910262