-
 Tel:86-15176910262
-

Search
 Tel:86-15176910262
Search
An accumulator is one of the most important auxiliary systems in a modern ERW tube mill. It stores steel strip temporarily between the coil processing section and the forming mill, allowing the tube mill to continue producing while the incoming steel coil is being replaced or joined.
Choosing the right tube mill accumulator is important for maintaining continuous production, reducing downtime, and maximizing the overall efficiency of an ERW tube mill.
However, not every accumulator is suitable for every tube mill.
The correct accumulator should be selected according to the tube mill's strip width, material thickness, production speed, coil weight, coil dimensions, and required strip storage capacity.
In this guide, we explain the main types of tube mill accumulators, how they work, and how to select the right accumulator for your ERW tube production line.
A tube mill accumulator is a strip storage system installed between the coil preparation section and the forming section of an ERW tube mill.
Its main function is to store a certain length of steel strip and continuously feed the forming mill while a new coil is being prepared.
A typical ERW tube production process is:
Uncoiler → Strip Processing → Accumulator → Forming Mill → HF Welding → Sizing → Cutting
When the current coil is almost finished, the strip coming from the accumulator continues feeding the forming mill.
At the same time, the operator or automatic system can:
Stop the uncoiler
Cut the finished coil
Load a new coil
Connect the new coil
Restart strip feeding
This allows the forming and welding sections to continue operating without stopping.

Without an accumulator, the entire tube mill would normally need to stop whenever the steel coil was replaced.
For a high-speed tube mill, this can result in significant production losses.
An accumulator provides several important benefits.
The forming and welding sections can continue operating while a new coil is being prepared.
This is especially important for high-speed ERW tube mills.
A properly sized accumulator provides enough stored strip to cover the coil change and strip joining process.
Reducing the number of mill stops can significantly increase the actual production output over a working shift.
Modern accumulators can be integrated with the tube mill's PLC and automatic coil handling system.
Several accumulator designs are used in ERW tube mills.
The most common types include:
Horizontal Spiral Accumulator
Vertical Spiral Accumulator
Cage Accumulator
Loop-Type Accumulator
The best choice depends on the tube mill design and production requirements.
A cage accumulator stores strip by forming multiple loops inside a cage structure.
The strip enters the accumulator continuously and is stored in multiple loops.
When the forming mill requires material, the stored strip is released continuously toward the forming section.
Compact design
High storage capacity
Suitable for many ERW tube mills
Relatively simple operation
Suitable for medium and high-speed production
Cage accumulators are commonly used where space and production efficiency are important considerations.

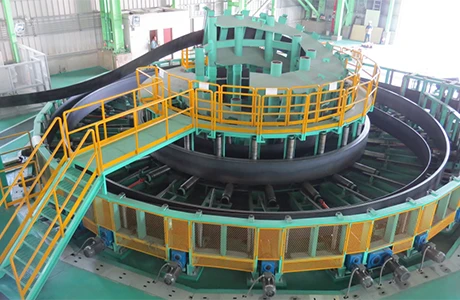
A spiral accumulator stores the strip in a spiral configuration.
The strip is continuously fed into the accumulator and stored along the spiral path.
When the forming mill requires material, the strip is continuously released.
Spiral accumulators can provide high storage capacity and are suitable for high-speed tube production.
High strip storage capacity
Suitable for high-speed tube mills
Smooth strip handling
Continuous strip feeding
Good production efficiency

The physical layout of the accumulator is also important.
A horizontal accumulator stores the strip primarily along the horizontal direction.
Convenient maintenance
Easier access
Suitable for factories with sufficient floor space
Good for many standard tube mill configurations
The main limitation is that it may require a relatively long installation area.
A vertical accumulator uses the available vertical space to store strip.
Smaller floor footprint
Useful when factory floor space is limited
Can provide substantial strip storage
However, the supporting structure and strip handling system must be carefully designed.
One of the most important parameters when selecting an accumulator is storage capacity.
The accumulator must contain enough strip to keep the tube mill running while the coil is changed and the new strip is welded to the previous strip.
For example, assume:
Tube mill speed: 60 m/min
Coil change and strip joining time: 3 minutes
The accumulator should provide at least:
60 × 3 = 180 meters
of effective strip storage.
In practice, additional capacity is normally recommended to provide a safety margin.
The actual required capacity depends on:
Tube mill speed
Coil change time
Strip joining time
Coil handling method
Operator efficiency
Automation level
Production speed has a direct impact on accumulator requirements.
For example:
| Tube Mill Speed | Coil Change Time | Minimum Effective Storage |
|---|---|---|
| 30 m/min | 3 min | 90 m |
| 40 m/min | 3 min | 120 m |
| 60 m/min | 3 min | 180 m |
| 80 m/min | 3 min | 240 m |
| 100 m/min | 3 min | 300 m |
These values are simplified examples. The actual accumulator capacity should be determined according to the complete production line design.
As production speed increases, the accumulator needs to provide more stored strip for the same coil-change time.
Before selecting an accumulator, you should provide the equipment manufacturer with several key parameters.
The accumulator must be designed for the maximum strip width used by the tube mill.
Strip width is determined by the tube diameter, wall thickness, and forming method.
Thicker strip requires stronger mechanical components and may affect the accumulator's storage capacity and operating speed.
Different materials have different mechanical properties.
For example:
Carbon steel
High-strength steel
Stainless steel
Galvanized steel
may require different strip handling and tension control configurations.
The accumulator must be capable of handling the maximum strip speed of the tube mill.
Maximum coil weight affects the design of the uncoiler and strip entry system.
Although coil weight does not directly determine accumulator capacity, it is important for the complete coil preparation section.
Storage length should be calculated based on line speed and coil change time.
The available installation area can determine whether a horizontal, vertical, cage, or spiral accumulator is most suitable.
A simple starting point is:
Required Storage Length = Tube Mill Speed × Coil Change Time
For example:
If the tube mill runs at 80 m/min and the coil change process requires 4 minutes:
80 × 4 = 320 meters
The accumulator should therefore provide more than 320 meters of effective storage capacity.
A safety margin should normally be considered because actual coil changing time can vary.
Storage capacity is not the only consideration.
The accumulator must also maintain stable strip tension.
Poor tension control can cause:
Strip deformation
Edge damage
Strip wandering
Forming instability
Welding problems
Tube dimensional problems
A good accumulator should provide smooth strip feeding and stable tension between the entry section and forming mill.
Although the accumulator is located before the forming section, its performance can indirectly affect the welding process.
If strip tension fluctuates significantly, the forming section may experience unstable strip movement.
This can affect:
Edge alignment
Forming accuracy
Welding stability
Tube dimensions
Therefore, accumulator performance should be considered as part of the complete ERW tube mill system rather than as an independent machine.
Modern tube mills can use different levels of automation.
Operators control important operations manually.
This solution may be suitable for:
Low production capacity
Smaller tube mills
Lower investment projects
The accumulator and coil preparation section are integrated with the PLC.
The system can automatically control:
Strip feeding
Strip storage
Speed synchronization
Coil change
Strip joining
Tension control
Automatic systems are particularly valuable for high-speed production lines.

Different tube mill sizes have different requirements.
For small-diameter tubes and relatively low production speeds, a compact accumulator may be sufficient.
Medium-size ERW tube mills generally require a larger storage capacity and stronger strip handling system.
Large-diameter and high-speed tube mills require high-capacity accumulators with robust mechanical structures and reliable tension control.
For large production lines, accumulator design should be closely integrated with the forming mill, HF welder, and coil preparation system.

Even a correctly designed accumulator requires proper operation and maintenance.
Common problems include:
Possible causes:
Incorrect alignment
Uneven tension
Damaged rollers
Improper setup
Possible causes:
Damaged rollers
Foreign material
Incorrect strip path
Excessive contact pressure
Possible causes:
Accumulator capacity too small
Coil change time too long
Production speed too high
Possible causes:
Incorrect speed synchronization
Control system problems
Mechanical resistance
Improper setup
Regular maintenance can improve reliability and extend equipment life.
Important maintenance tasks include:
Inspecting rollers
Checking bearings
Checking drive systems
Lubricating moving components
Inspecting strip alignment
Checking sensors
Checking electrical connections
Inspecting safety devices
Checking tension control
Cleaning accumulated steel debris
For high-speed production lines, preventive maintenance is particularly important.

When comparing accumulator suppliers, don't focus only on price.
Consider:
The manufacturer should understand the complete ERW tube production process.
The accumulator should work smoothly with:
Uncoiler
Shear & End Welder
Forming Mill
HF Welder
PLC Control System
Confirm that the accumulator is designed for the required maximum line speed.
Technical support, spare parts, installation, and commissioning are important for long-term operation.
At HEBEI AIS MACHINERY, accumulator selection is based on the complete ERW tube mill configuration rather than a standard one-size-fits-all design.
We consider:
Tube diameter
Wall thickness
Strip width
Steel grade
Production speed
Coil weight
Required storage capacity
Factory layout
Automation requirements
Depending on the project, we can provide suitable accumulator solutions integrated with the complete tube mill production line.
Our ERW tube mill solutions can include:
Uncoiler
Strip End Shear & Welder
Accumulator
Forming Mill
HF Welder
Impeder
Squeeze Rolls
Cooling Section
Sizing Mill
Cutting Machine
Online Inspection System
Choosing the right tube mill accumulator is essential for achieving continuous and efficient ERW tube production.
The correct accumulator should provide sufficient strip storage to cover coil changes while maintaining stable strip tension and smooth feeding to the forming mill.
When selecting an accumulator, manufacturers should consider production speed, strip width, material thickness, coil specifications, required storage capacity, available factory space, and automation requirements.
For high-speed ERW tube mills, a properly designed accumulator can significantly reduce downtime and improve overall production efficiency.
The best solution is not necessarily the accumulator with the largest capacity. It is the system that is correctly matched to the complete tube mill production line.
A tube mill accumulator stores steel strip temporarily so that the forming and welding sections can continue operating while a new coil is being prepared and joined.
As a starting point, multiply the tube mill's strip speed by the required coil change time. Additional capacity should normally be considered as a safety margin.
A cage accumulator stores strip through multiple loops inside a cage structure, while a spiral accumulator stores strip along a spiral path. The best choice depends on production speed, capacity, layout, and tube mill configuration.
No. An oversized accumulator increases equipment cost and installation requirements. The capacity should be matched to production speed and coil change time.
Yes. Modern accumulators can be integrated with the tube mill PLC and automatic coil handling system.
Indirectly, yes. Stable strip feeding and tension help maintain consistent forming and edge alignment, which can contribute to stable welding and tube dimensions.
Maintenance intervals depend on the machine design and operating conditions. Regular inspection of rollers, bearings, drives, sensors, alignment, and tension systems is recommended.
Send a Message
Dear customer, thank you for your attention! We provide high-quality machinery and equipment and look forward to your orders. Please inform us of your needs and we will respond quickly!