-
 Tel:86-15176910262
-

Search

Buying a Steel Slitting Line? 8 Key Specifications You Should Know
Aug . 12, 2026 10:17
1. What Is a Steel Slitting Line? ⚙️
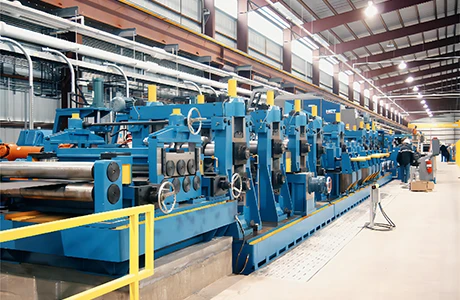
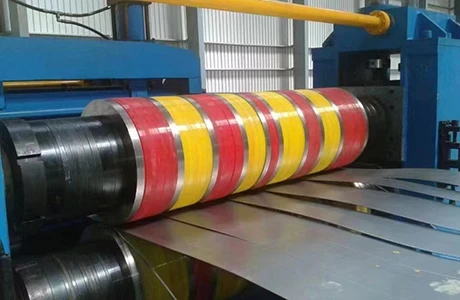
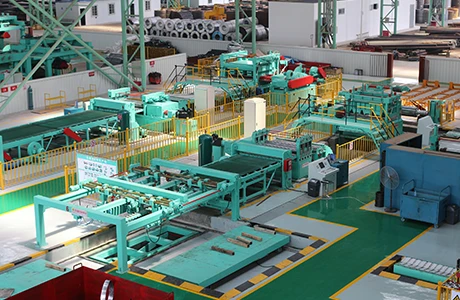
A steel slitting line continuously unwinds a master coil, cuts it longitudinally into several narrower strips, separates the strips and recoils them into individual slit coils.
A typical process is:
👉Loading → Decoiling → Leveling → Slitting → Scrap Edge Winding → Strip Separation → Tensioning → Recoiling → Coil Unloading
The main purpose is to convert a wide master coil into narrow steel strips suitable for the next production process.
For example:
Master Coil:
1,250 mm wide ➡️ Slitting ➡️ 50 mm + 50 mm + 80 mm + 100 mm + 150 mm + ...➡️ Multiple Narrow Steel Coils
The exact slitting pattern depends on the customer's required strip widths and the material utilization.
2. What Materials Can Be Processed?
A Steel Coil Slitting Line can be designed for different steel materials. The material type is one of the first factors that should be confirmed before selecting the machine.
Common materials include:
| Material | Typical Application |
|---|---|
| Hot Rolled Steel (HR) | Structural pipes, general steel tubes, construction products |
| Cold Rolled Steel (CR) | Precision tubes, furniture tubes, automotive and general fabrication |
| Galvanized Steel (GI/HDG) | Galvanized pipes, construction products, HVAC and other applications |
| Stainless Steel | Decorative tubes, food equipment, industrial pipes |
| Electrical / Silicon Steel | Transformer and electrical applications |
| High-Strength Steel | Automotive and structural applications |
For example, ASTM A1011 covers hot-rolled carbon, structural, HSLA and other steel sheet and strip products, while ASTM A1008 covers cold-rolled carbon, structural, HSLA and other steel sheet and strip products.
Important: “HR steel”, “CR steel” or “galvanized steel” describes the material/product condition, but the actual machine design should also consider yield strength, tensile strength, thickness, surface condition and required slit quality.
3. Steel Coil Width and Thickness
The maximum coil width and thickness are two of the most important specifications of a slitting line.
📈For example, a customer may require:
- Coil Width: 1,000–1,600 mm
- Coil Thickness: 0.5–3.0 mm
- Coil Weight: 20 tons
- Slit Width: 30–500 mm
- Maximum Slitting Speed: 120 m/min
The machine must be selected according to the maximum material specification, not only the average material you normally purchase.
For example, if your normal production is 1.2 mm × 1,250 mm but you occasionally need to process 3.0 mm × 1,600 mm coils, the slitting line must be designed for the 3.0 mm × 1,600 mm requirement.
Commercial slitting lines are available in significantly different capacities. For example, some 1,600 mm lines are designed for approximately 0.3–4 mm material and up to 25 tons, while larger systems can be designed around 2,000 mm width and 30 tons or more. These are examples rather than universal standards; the actual specification depends on the machine design.
4. How Is Strip Width Related to Pipe Diameter? 📏
This is one of the most important questions for customers who purchase a slitting line for ERW Tube Mill production.
For a round pipe, the required strip width is related approximately to the circumference of the finished tube.
📌A simple reference relationship is:
Strip Width ≈ π × Tube Diameter
However, this should not be treated as an exact production formula.
The actual strip width is affected by:
- • Tube diameter
- • Wall thickness
- • Material
- • Forming method
- • Tube mill design
- • Required dimensional tolerance
Therefore, the final strip width should always be confirmed by the tube mill manufacturer according to the specific roll forming design.


5. Does Wall Thickness Affect Strip Width?
Yes, but it is important to understand the relationship correctly.
For the same nominal tube diameter, changing the wall thickness does not normally mean that the strip width changes dramatically according to a simple fixed formula.
For example, a customer may produce:
- Ø50 × 1.0 mm
- Ø50 × 1.5 mm
- Ø50 × 2.0 mm
The tube diameter is the same, but the material thickness is different.
The strip width should therefore be determined according to the actual tube mill forming design, rather than simply calculating the width from diameter and thickness using a universal formula.
This distinction is important when purchasing a slitting line for tube production.
6. Typical Strip Widths for Tube Production
For ERW tube manufacturers, the required slit width depends mainly on the tube sizes being produced.
🔍A practical way to think about the relationship is:
Small Tube → Narrow Strip
Large Tube → Wider Strip
For example, a tube mill producing small-diameter tubes may require strips around several tens of millimeters wide, while larger tube mills may require strips several hundred millimeters wide.
Therefore, if a customer tells us:
“I want to produce tubes from Ø20 mm to Ø76 mm.”
we cannot select the slitting line based only on the 76 mm tube diameter.
We also need to know:
- Wall thickness
- Material
- Number of tube sizes
- Required strip widths
- Master coil width
- Coil thickness
- Coil weight
The complete slitting pattern can then be calculated.


7. Coil Weight: How Important Is It? ⚖️
Coil weight is another key parameter when selecting a slitting line.
The machine needs to be able to safely load, unwind and rewind the required coil weight.
A larger coil weight normally means higher requirements for:
- Loading car
- Decoiler
- Hydraulic expansion
- Slitter stand
- Recoiler
- Tension unit
- Coil unloading system
For example, a commercially available 1,600 mm slitting line can be configured around 15-ton capacity, while larger configurations can be designed for 20–40 tons.
8. How to Choose the Right Slitting Line? 🔍
Choosing a slitting line should not start with:
“I need a 1,600 mm slitting machine.”
Instead, start with:
“What products do I want to manufacture?”
This is especially important for customers producing ERW pipes and tubes.
Step 1 — Confirm the Tube Diameter Range
For example:
Ø20–Ø76 mm or Ø50–Ø165 mm
The maximum tube diameter affects the required strip width.
Step 2 — Confirm Wall Thickness
For example:
0.8–2.0 mm or 1.5–4.0 mm
Thickness affects the slitting machine's cutting capacity and mechanical design.
Step 3 — Confirm Material
Tell the manufacturer whether you will process:
- Hot Rolled Steel
- Cold Rolled Steel
- Galvanized Steel
- Stainless Steel
- High-Strength Steel
- Electrical Steel
Different materials can have significantly different mechanical properties and surface requirements.
Step 4 — Confirm Master Coil Width
Common master coil widths may include:
1,000 mm / 1,250 mm / 1,500 mm / 1,600 mm / 1,800 mm / 2,000 mm
But the correct choice depends on the coils available from your steel supplier.
There is no advantage in buying a 2,000 mm slitting line if your steel supplier only provides 1,250 mm coils and your production does not require wider material.
Step 5 — Confirm Required Slit Width
This is particularly important for tube production.
For example:
Tube A requires approximately 80 mm strip
Tube B requires approximately 120 mm strip
Tube C requires approximately 180 mm strip
Tube D requires approximately 250 mm strip
The slitting line should be able to produce these widths efficiently.
Step 6 — Confirm Maximum Coil Weight
For example:
Maximum Coil Weight: 15,000 kg
or
Maximum Coil Weight: 25,000 kg
The decoiler, recoiler, loading car and other components must all be designed for the required weight.
Step 7 — Consider Production Speed
Higher line speed can improve productivity, but maximum speed should not be considered independently.
Actual production speed is affected by:
- Material thickness
- Material strength
- Strip width
- Number of slits
- Coil weight
- Slitting quality
- Recoiling requirements

Related Products




Related News

2026-08-18 09:42:30
August Promotion at AIS Machinery – Complete Solutions for ERW Tube Mills & Steel Processing
AIS Machinery August Promotion is here! We are offering competitive prices on ERW Tube Mills, Slitting Lines, Cut-to-Length Lines, Cold Roll Forming Machines and Tube Mill Spare Parts. Whether you are planning a new tube production line, upgrading existing equipment, or looking for reliable spare parts, we can provide a complete solution. Our professional engineers offer technical support from machine selection to production, installation and after-sales service. Contact AIS Machinery this August and let us help you find the right equipment for your project.

2026-08-17 09:43:30
C U Purlin Roll Forming Machine | Flexible C/U Profile Production
CU Profile Roll Forming Machine is designed to continuously produce C and U-shaped steel profiles from metal coils. The complete line can include a decoiler, leveling and feeding system, punching unit, roll forming machine, cutting system and run-out table. Depending on production requirements, the machine can use manual C/U changeover or computer-controlled automatic size adjustment. It is suitable for producing C/U channels, structural profiles, framing components and other steel sections with consistent dimensions and reliable production efficiency.

2026-08-13 10:50:44
Double Head Uncoiler for Tube Mills: Continuous Coil Loading and Faster Production
Double Head Uncoiler is an efficient coil feeding machine designed for ERW tube mills, pipe mills, and coil processing lines. With two hydraulic expanding mandrels, it allows one steel coil to run while the next coil is prepared, reducing coil changeover time and production downtime. The hydraulic drive provides stable and reliable coil unwinding, making the double head uncoiler an ideal solution for medium and large-size tube mills, heavy steel coils, and high-production applications.

2026-08-12 10:17:44
Buying a Steel Slitting Line? 8 Key Specifications You Should Know
Looking for a reliable Steel Slitting Line for your tube or pipe production? Our Coil Slitting Machine is designed to convert wide steel coils into accurate narrow strips for ERW Tube Mills, roll forming lines and other applications. From HR, CR and galvanized steel to different coil widths, thicknesses and weights, the slitting line can be customized to your requirements. ⚙️ Learn how to select the right slitting capacity, strip width, coil weight and production speed for your business.

2026-08-11 09:25:01
Conveyor and Run Out Table for ERW Tube Mill | Pipe Conveying & Discharge System
Conveyor and Run Out Table is an important pipe handling system in an ERW Tube Mill, mainly installed after the flying saw or cold saw. It supports, conveys, aligns, buffers, and discharges finished pipes smoothly to the next process. A properly designed run out table can reduce manual handling, protect pipe surfaces, and improve production efficiency. With customized roller layout, conveying speed, table length, and discharge design, it can be matched with different pipe sizes, production speeds, and downstream stacking or packing systems.

2026-08-10 10:07:47
3 Inch–5 Inch Tube Mill: The Most Popular Size Range for ERW Pipe Production
3–5 Inch ERW Tube Mill is one of the most popular choices for steel pipe manufacturers. This tube mill size range is widely used for producing round, square, and rectangular steel tubes for construction, machinery, furniture, automotive, and structural applications. With flexible tube diameter and wall thickness options, a 3 inch, 4 inch, or 5 inch tube mill can meet different production requirements. Learn how to choose the right ERW tube mill based on your products, target market, production speed, and future demand.

2026-08-06 09:50:37
Cold Roll Forming Machine with Punching: A Complete Guide for Custom Metal Profiles
A Cold Roll Forming Machine with Punching combines precision roll forming and automatic punching in one efficient production line. It can produce C channels, U channels, garage door struts, solar mounting profiles, and many other custom steel sections with round holes, slots, or special cutouts. The punching system improves production efficiency, reduces secondary processing, and ensures accurate hole positioning. AIS Machinery provides customized roll forming solutions based on your profile drawings and production requirements.

2026-08-05 09:48:14
Automatic vs Semi Automatic Shear and Welder: Which Coil Joining System Is Best for Your Tube Mill?
Our Automatic and Semi Automatic Shear and Welder systems are designed for reliable coil joining in ERW tube mills. Both machines use TIG welding technology to produce strong, smooth butt welds that pass easily through the accumulator and forming section. Whether you need a fully automated solution for high-volume production or a cost-effective semi automatic model, AIS Machinery offers customized systems to match different strip widths, thicknesses, and production capacities.
Send a Message
Dear customer, thank you for your attention! We provide high-quality machinery and equipment and look forward to your orders. Please inform us of your needs and we will respond quickly!
 English
 Albanian
 Arabic
 French
 German
 Indonesian
 Italian
 Japanese
 Kazakh
 Korean
 Latin
 Macedonian
 Portuguese
 Russian
 Spanish
 Thai
 Turkish
 Ukrainian
 Uzbek