-
 Tel:86-15176910262
-

Search
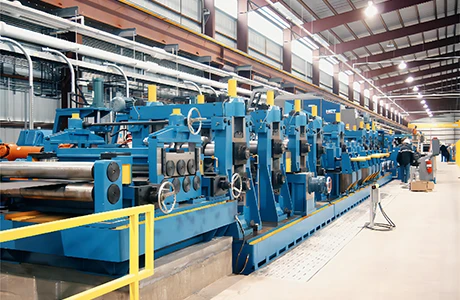

Horizontal vs Vertical vs Cage vs Disc Accumulator for ERW Tube Mills
Nov . 26, 2025 00:00
📘 Introduction
In an ERW tube mill, the accumulator ensures continuous strip feeding during coil changes, keeping the mill running without stoppage. The most common types are Horizontal Spiral, Vertical Spiral, Cage (Loop Cage), and Disc Accumulators. Each design fits different production speeds, strip sizes, and factory layouts.
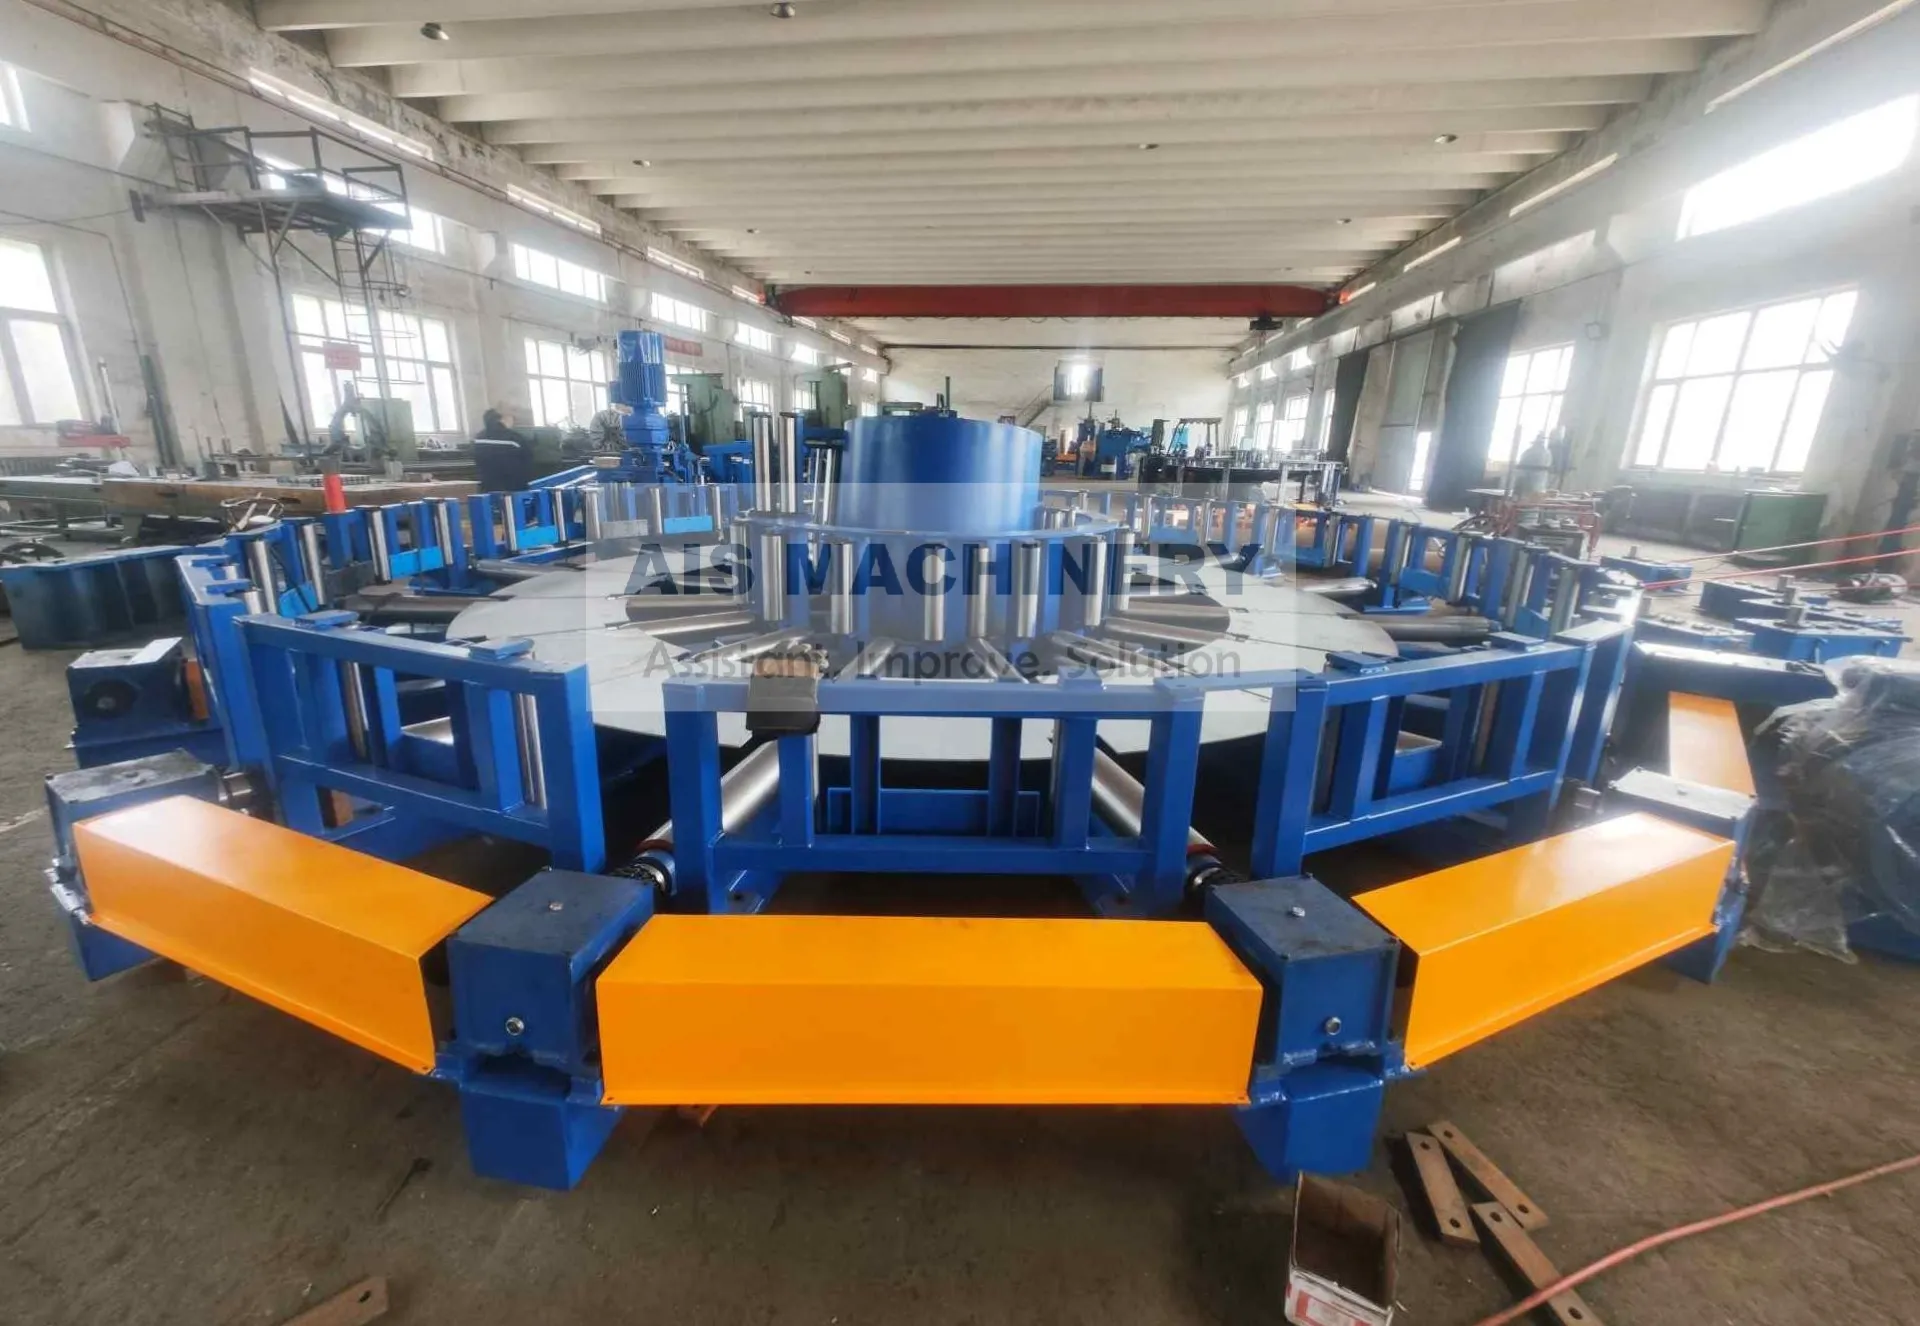
1. Horizontal Spiral Accumulator
-
Structure: Strip forms a horizontal spiral on a circular track; a movable trolley adjusts coil diameter.
-
Storage Capacity: 150–400 m
-
Line Speed: 120–180 m/min
-
Best For: Medium-speed ERW lines, structural and mechanical tubing
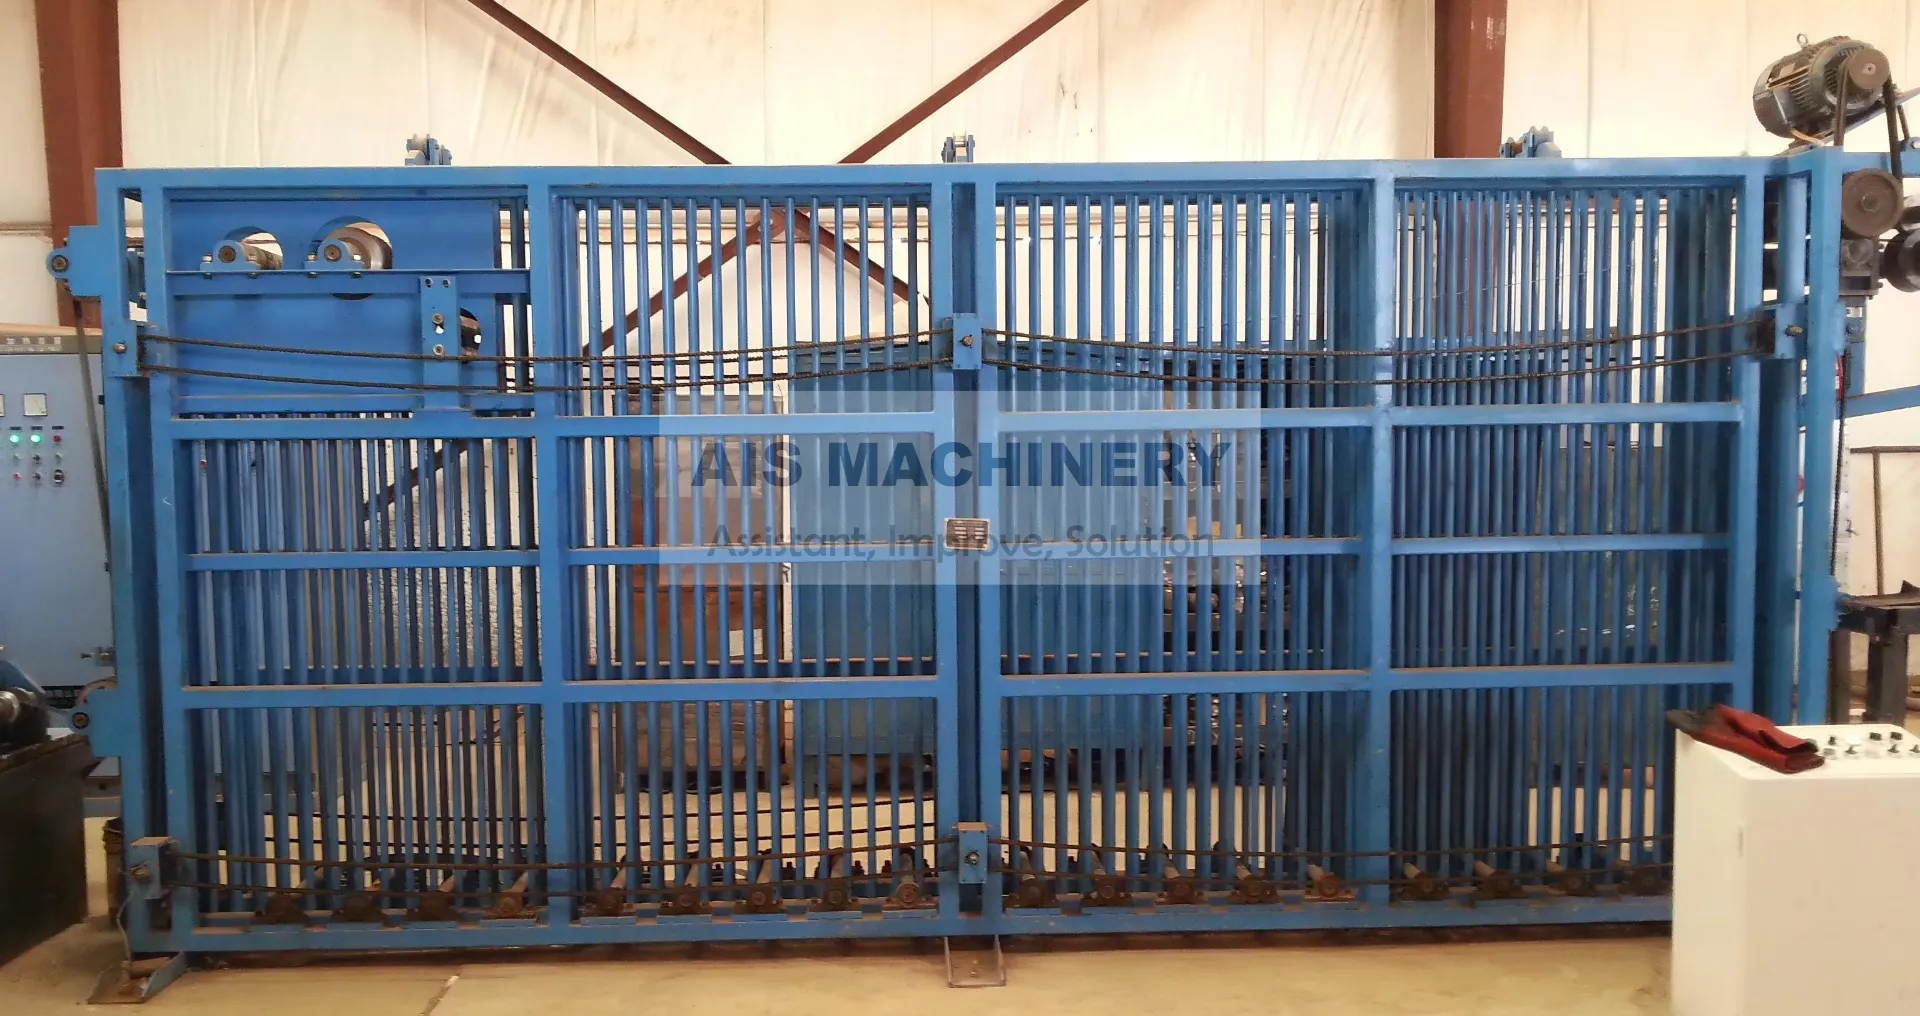
2. Vertical Spiral Accumulator
-
Structure: Strip forms vertical spiral layers; height is utilized to increase storage capacity.
-
Storage Capacity: 300–600 m
-
Line Speed: 150–250 m/min
-
Best For: Medium-to-high-speed lines, wide strip, medium-to-large tubes
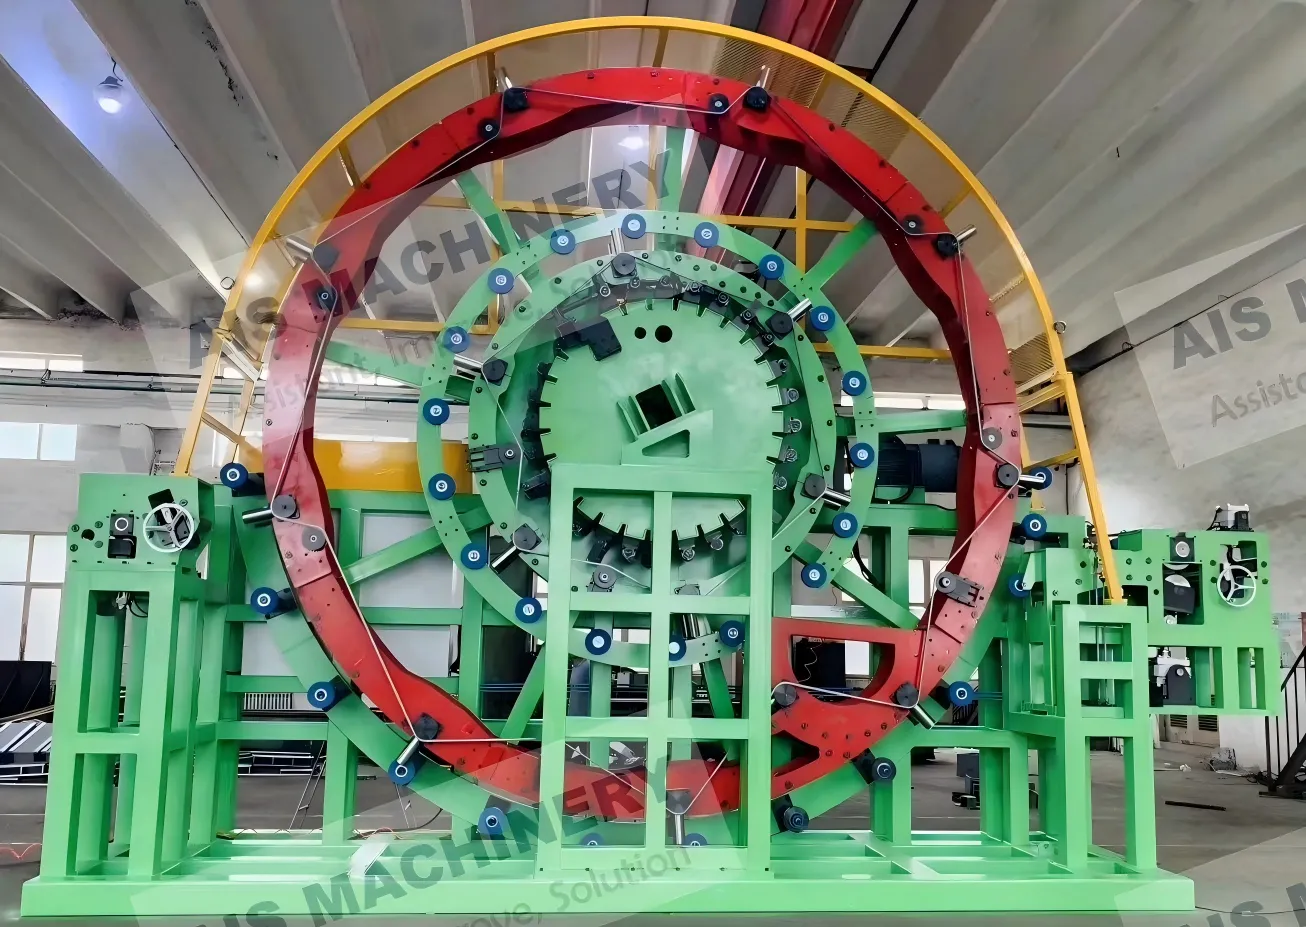
3. Cage Loop Accumulator
-
Structure: Strip passes through rotating cages to create large vertical loops with precise tension control.
-
Storage Capacity: 300–700+ m
-
Line Speed: 180–300+ m/min
-
Best For: High-speed lines, API pipe, automotive tube, continuous production
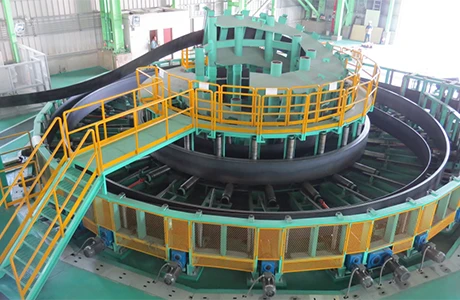
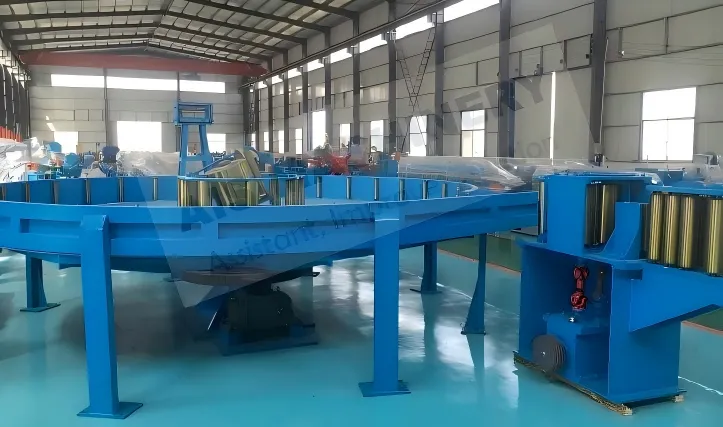
4. Disc Type Spiral Accumulator
-
Structure: Strip is wound into a flat spiral on a rotating disc for compact storage.
-
Storage Capacity: 80–250 m
-
Line Speed: 80–150 m/min
-
Best For: Small OD, thin-wall tubes, compact workshops
Detailed Performance Comparison
1. Strip Handling & Tension Control
| Type | Tension Control | Suitable Material | Characteristics |
|---|---|---|---|
| Disc | ★★☆☆☆ | Thin, low-strength steel | Simple structure; short strip path; sensitive to tension fluctuations |
| Horizontal Spiral | ★★★☆☆ | Carbon steel | Stable tension control; good for medium-speed lines |
| Vertical Spiral | ★★★★☆ | Wide, medium-thick strip | Vertical path reduces lateral fluctuations; larger storage |
| Cage Loop | ★★★★★ | High-strength, wide strip | Independent tension zones; highest precision |
2. Line Speed Capability
-
Disc: 80–150 m/min
-
Horizontal Spiral: 120–180 m/min
-
Vertical Spiral: 150–250 m/min
-
Cage Loop: 180–300+ m/min
Conclusion: For welding speeds >250 m/min, Cage Loop is the only reliable choice.
3. Storage Capacity & Buffer Efficiency
| Type | Storage Density | Max Capacity | Application |
|---|---|---|---|
| Disc | ★★★☆☆ | 80–250 m | Small tubes / small lines |
| Horizontal Spiral | ★★★☆☆ | 150–400 m | Medium output lines |
| Vertical Spiral | ★★★★☆ | 300–600 m | High-speed, frequent coil change |
| Cage Loop | ★★★★★ | 300–700+ m | Continuous high-speed production |
4. Floor Space & Height Requirements
| Type | Floor Area | Height | Foundation Requirement |
|---|---|---|---|
| Disc | Minimal | Low | Simple |
| Horizontal Spiral | Medium (larger diameter) | Low | Simple |
| Vertical Spiral | Small | High | Medium |
| Cage Loop | Medium | High | High (steel frame required) |
Key Notes:
-
Low building height → Horizontal / Disc
-
Limited floor space → Vertical / Cage
5. Engineering Reliability
-
⚙️Disc: Simple, limited application
-
⚙️Horizontal Spiral: Stable, low maintenance
-
⚙️Vertical Spiral: More complex, better performance
-
⚙️Cage Loop: Maximum continuous stability, suitable for 24/7 operation
Professional Selection Guide
➡️Step 1: Define Target Welding Speed
-
≤150 m/min → Disc / Horizontal
-
150–250 m/min → Vertical Spiral
-
≥250 m/min → Cage Loop
➡️Step 2: Evaluate Strip Specifications
-
Thin strip ≤1.2 mm → Disc / Horizontal
-
Wide strip >500 mm or thick >3 mm → Vertical / Cage
-
High-strength steel → Cage Loop
➡️Step 3: Consider Pipe Size
-
Small OD ≤60 mm → Disc
-
Small-medium OD ≤89 mm → Horizontal Spiral
-
Medium-large OD ≤168 mm → Vertical Spiral
-
Large or API OD ≥219 mm → Cage Loop
➡️Step 4: Analyze Workshop Layout
-
Low building → Horizontal / Disc
-
Narrow building → Vertical / Cage
-
No pit foundation → Disc / Horizontal
➡️Step 5: Balance Budget vs Performance
-
Economical → Disc Type
-
High cost-performance → Horizontal Spiral
-
High-speed stability → Vertical Spiral
-
Continuous high-end production → Cage Loop

Related Products





Related News

2026-11-02 02:23:25
ERW Pipe Mill for Sale: Buyer FAQs for a 76 mm Line
Review the 21.3 mm to 76 mm range, materials, equipment, speed, power, cutting methods, and production controls for an ERW pipe mill for sale.

2026-10-29 00:44:48
High-Speed Steel Coil Slitting Line FAQ: Specifications, Ordering and Support Questions
Get direct answers about High-Speed Steel Coil Slitting Line specifications, material compatibility, component layout, process steps, quality standards, and after-sales support from HEBEI AIS MACHINERY EQUIPMENT CO.,LTD.

2026-10-28 00:06:34
Learn the key working requirements and integration criteria for selecting a steel pipe making machine manufacturer. Covers diameter range, wall thickness, strip grade, HF welding power, footprint, and electrical supply using the 10inch 273mm ERW Pipe Making Machine from HEBEI AIS MACHINERY EQUIPMENT CO.,LTD.

2026-10-28 00:05:55
Choosing a Flying Cold Saw: Working Requirements and Integration Fit
Learn the key selection criteria for a flying cold saw — pipe diameter, line speed, cut precision, blade type, and PLC integration — to find the right cold cutting flying saw machine for your ERW tube mill.

2026-10-28 00:05:28
Evaluate whether the GGP 100kw Solid State High Frequency Induction Heating Welding Machine fits your ERW pipe production line. This guide covers power requirements, cooling infrastructure, electrical supply, and control integration criteria.

2026-10-28 00:04:41
Choosing Quick-Change System for Forming & Sizing Section: Application Fit and Specification Checks
Learn the key selection criteria for a Quick-Change System for Forming & Sizing Section in ERW tube mills — covering changeover frequency, cassette structure, pneumatic couplings, and application scope for structural, automotive, and export tube production.

2026-10-23 17:54:55
Compare a steel pipe seam annealing machine and a pipe threading machine: function, published ranges, PLC/HMI and CNC controls, operating steps and maintenance.

2026-10-04 16:13:15
HEBEI AIS MACHINERY at Tube & Wire Shanghai 2026 | Tube Mill Solutions
HEBEI AIS MACHINERY participated in Tube & Wire Shanghai 2026, meeting new and long-term customers to discuss ERW tube mills, steel processing equipment, new projects, and future cooperation.
Send a Message
Dear customer, thank you for your attention! We provide high-quality machinery and equipment and look forward to your orders. Please inform us of your needs and we will respond quickly!
 English
 Albanian
 Arabic
 French
 German
 Indonesian
 Italian
 Japanese
 Kazakh
 Korean
 Latin
 Macedonian
 Portuguese
 Russian
 Spanish
 Thai
 Turkish
 Ukrainian
 Uzbek